
Grade Grade DM Grade 2 735A50 Wire for, Brand Usha Martin, Diameter 030 to 1600 mm
Active
Premium
Key Highlights
$ 0.70
per Gram (g)
MOQ
1
Available Variants
Technical Specifications
| Parameter | Value |
|---|---|
| Brand | Usha Martin |
| Grade | Grade DM / Grade 2 |
| Diameter | 0.30 to 16.00 mm |
| Material | High Carbon Spring Steel |
| Surface Finish | Oiled and Black |
| Usage/Application | Automobile Spring |
Product Description
Optimized Use of Grade DM Grade 2 735A50 Wire in High-Volume Industrial Applications
Chemical makeup with standard analysis in percentage: ccrmnvsips 0. 50, 0. 55, 1. 00, 1. 20, 0. 70, 0. 80, 0. 15, 0. 25, 0. 35, And a maximum of 0. 35. This is Ventura EN47 chromium vanadium spring steel provided in its rolled state as well as the spheroidized annealed state, En47 is ideal for oil hardening and subsequent tempering. It is effective when utilized in the oil-hardened process The en47 spring steel, When tempered, Merges spring-like properties with impressive resistance to wear and abrasion. In its hardened state, En47 delivers outstanding performance Durability and shock absorption properties that render it an ideal alloy spring steel for components subjected to stress surprise and, To emphasize vibration. Applications EN47 steels are notable for their excellent hardenability, Impressive hot robust overall, Working characteristics and strong, Mechanical properties resistance to decarburization A broad selection of including those, Essential springs for automobiles, Locomotives, And large plate springs, Primarily utilizes SUP10 material Designed for and industrial, Agricultural machinery, Robust vehicles loads, It addresses the stress levels and dimensions of both the larger plate spring and the helical spring finds extensive use in the automotive sector in addition to in various general ideal for, Engineering fields situations demanding high performance Exceptional resistance to stretching and durability make this material ideal designed for application in crankshafts, Steering knuckles, Gears, Spindles, And pumps. Forge at a temperature of 1050°C. Do not exceed this limit Process this steel when its temperature drops below 840°C; gradually heat to between 820 and 840°C, Ensuring adequate soaking. Allow for slow cooling afterward the furnace. We utilize an electric furnace for annealing to prevent decarburization. We gradually, For hardening preheat to 650/700 °C and Immerse completely, Then heat until reaching the final hardening temperature of 830/860°C, Ensuring the component is uniformly heated After quenching the en47 spring temper it, Steel part while the tools remain warm to the touch Heat to the tempering temperature, Then allow to soak for one hour for every 25 millimeters with a, Of thickness minimum soaking time of two hours, And cool in air afterward In general, The tempering range for this grade will fall between 400 and 600 °C, Encompassing heat treatment temperatures and heating rates The duration for cooling and soaking will differ derived from the dimensions and configuration of each part Factors to take into account during the heat treatment procedure encompass the furnace type, The quenching medium, And the equipment for transferring workpieces. We recommend you consult your Comprehensive heat treatment services offering expert advice on thermal processes processing of en47 material
Shipping Information
Availability
In Stock
Price
Excluding all taxes
Ships from
Mumbai
Delivery Location
All India delivery available
Shipping
As per delivery location
Seller Information
V
Mumbai, Maharashtra, India
Established:
1965
Delivery Time:
60+ Business Days
Shipping Options:
Trust & Safety
Trade Assurance Protected
Secure Payment Methods
Logistics Tracking Available
24/7 Customer Support

All Shapes High Carbon Spring Steel Wire Forms Online
Request Price
per Pc
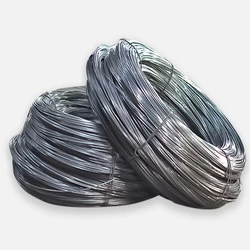
Carbon Steel Wire — Black Painting Surface Non Alloy
Request Price
per Pc
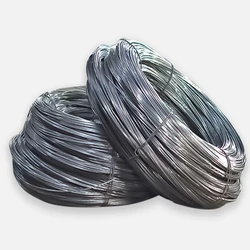
Carbon Steel Wire — Black painting surface treatment
Request Price
per Pc

Wire Forms Spring — 5 to 15 mm wire size polished
Request Price
per Pc
You May Also Like
Hb Wires
Mild Steel Wires
Spring Wire
Pc Strand
High Carbon Wire
Stay Wire
202 Stainless Steel Wire
Steel Wire Strand
Hhb Wire
High Tensile Steel Wire
Copper Coated Stainless Steel Wire
Carbon Steel Wires
Acsr Core Wires
Sealing Wire
High Carbon Spring Steel Wire
Steel Wire Wool
Fastener Wire
Aluminium Clad Steel Wire
Galvanized Steel Strand
Ungalvanized Steel Wire Rope
Lashing Wire
304 Stainless Steel Wire
Stainless Spring Wire
Stainless Steel Fine Wire
316 Stainless Steel Wire
Stainless Steel Cold Heading Wire
302 Stainless Steel Wire
Stainless Steel Wire Ties

HB Wire, UsageApplication Fasteners, Color Black
$ 475.02
per Metric Ton (t)

Application Industrial, Grade SAE 1018 HB Binding Wire, Length 500 mtr, Color Silver
$ 10.27
per Gram (g)

UsageApplication FOR MAUFACTURING BUCLES, WELDING RODS, J HOOKS, Color Silver Hard Bright Wire, Wire Size 1MM--8MM
$ 0.51
per Gram (g)

H B Wires, Material Galvanized Iron, Wire Gauge 12 SWG
$ 472.62
per Metric Ton (t)
You May Also Like